0102030405
High Functionality Transparent Polyethylene Sauce Packaging by China Suppliers | Acid & Alkali Resistant, Boiling Safe
Product Description
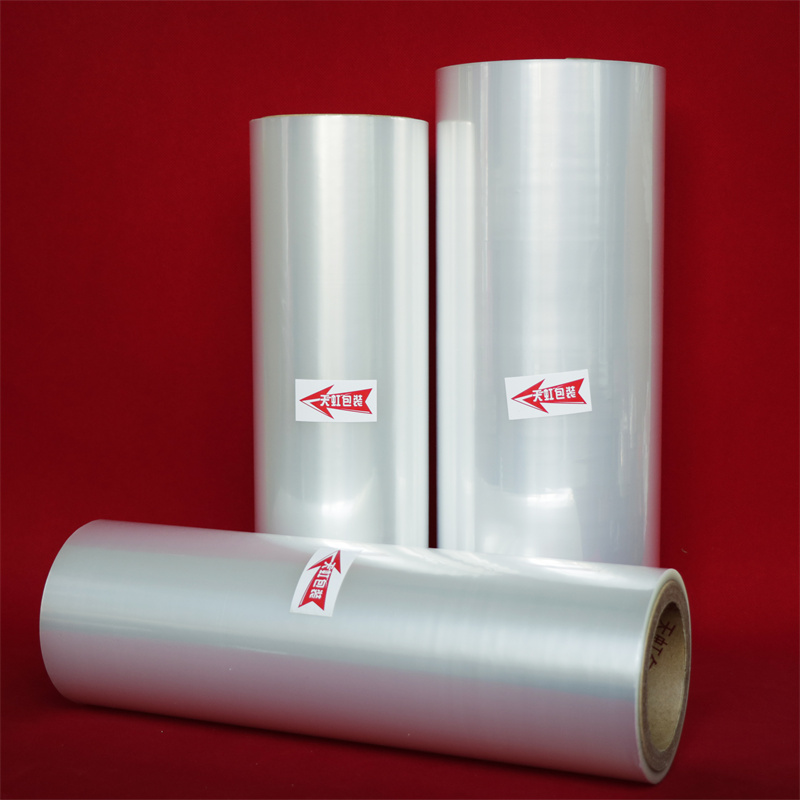
Sauce packaging fears leakage, boiled food packaging fears high-temperature deformation—traditional films often suffer from packaging damage due to insufficient corrosion resistance, liquid leakage due to low heat-sealing strength, or film surface shrinkage during boiling sterilization due to poor temperature resistance. Our high-functional IPE film integrates three core performances of "high-strength heat-sealing + acid-alkali corrosion resistance + wide temperature range tolerance" through multi-layer co-extrusion technology and special raw material formulation, providing a stable and reliable solution for sauce and boiled food packaging.
1
High-Strength Heat-Sealing: Reliable Protection Against Liquid Leakage
Using special heat-sealing resin and interlayer reinforcement technology, the film's heat-sealing strength is stably maintained at 20–25 N/15mm, far exceeding the industry's conventional standard of 15–18 N/15mm. Even when packaging thick sauces with particles (such as broad bean paste, beef sauce) or when internal pressure increases after boiling, the seal can still fit tightly without cracking or liquid leakage. Tests show that when the film bag containing sauce falls from a height of 1.2 meters or bears 5 kg of lateral pressure, the seal integrity rate reaches 100%, completely solving the leakage risk in sauce transportation and storage.
2
Acid-Alkali Corrosion Resistance: Suitable for Multiple Sauce Types
The film surface is added with chemical corrosion-resistant modifiers, forming a uniform protective layer through precision co-extrusion technology, which can withstand acid-alkali environments with pH 2–12 for a long time—whether it is acidic vinegar, tomato sauce, alkaline broad bean paste, or high-salt soy sauce and chili sauce, it can effectively block the penetration of sauce components, preventing the film from swelling, discoloration or strength attenuation. Even if the sauce is stored for a long time (more than 6 months), the packaging remains intact without affecting product quality and appearance.
3
Wide Temperature Range Resistance: Suitable for Boiling Sterilization Process
The raw material uses high-temperature resistant polyethylene substrate, which is subjected to special cross-linking treatment, expanding the film's temperature resistance range to -20℃ ~ 121℃: it can be used for frozen sauce storage at low temperatures, and can withstand 121℃ boiling sterilization at high temperatures (such as 10–30 minutes of boiling heating for prepared dishes). During the process, the film surface does not shrink or deform, and the heat-sealing strength attenuation rate is less than 5%. No additional protective layer is needed, directly adapting to the boiling packaging line of food factories, simplifying the production process and reducing packaging costs.
4
Safety Compliance and Efficient Processing: Balancing Practicality and Productivity
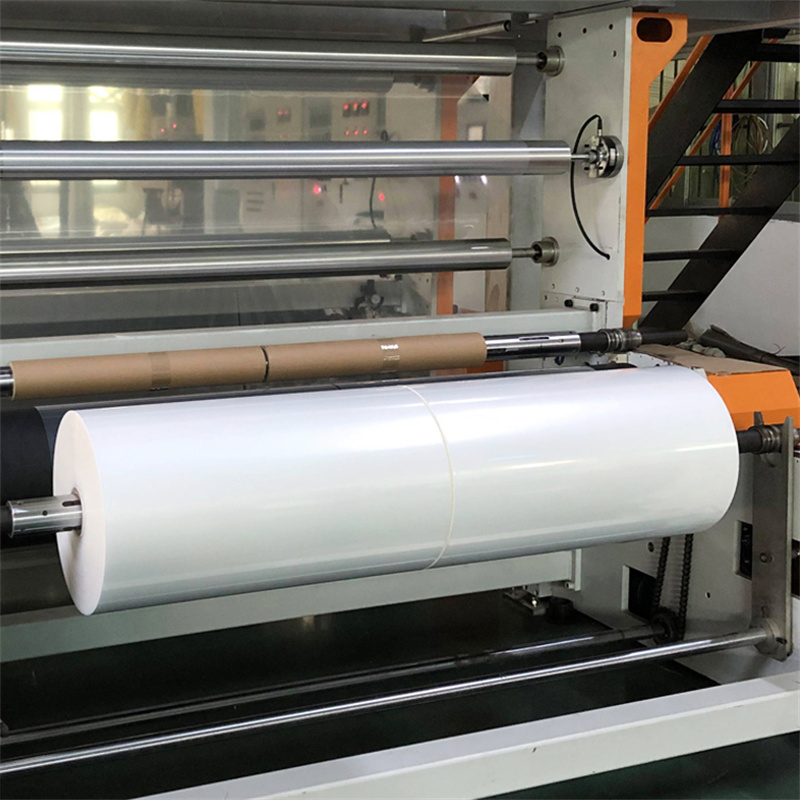
All raw materials comply with FDA and EU 10/2011 food contact standards, with no harmful substances precipitated during acid-alkali resistance and high-temperature resistance, and can directly contact food and sauces. The film surface has high flatness (thickness uniformity ±2 μm), compatible with high-speed automatic packaging machines of 80–180 bags per minute, ensuring smooth conveying without jamming and reducing downtime for debugging. It also supports surface printing (adhesion up to 4B level), and can customize brand logos and product information, helping to improve the visual texture of packaging and enhance consumer recognition.
Q1
What makes the IPE film's heat-sealing strength superior to conventional packaging films?
The IPE film uses special heat-sealing resin combined with interlayer reinforcement technology, achieving a heat-sealing strength of 20–25 N/15mm—significantly higher than the industry standard of 15–18 N/15mm. This ensures the seal remains intact even under drop impacts of 1.2 meters or lateral pressure of 5 kg, making it ideal for heavy or liquid-rich sauce packaging.
Q2
Which types of sauces is this IPE film compatible with?
The film is compatible with a wide range of sauce types, including acidic products (vinegar, tomato sauce), alkaline products (broad bean paste), and high-salt products (soy sauce, chili sauce). Its chemical corrosion-resistant modifier layer can withstand pH environments ranging from 2 to 12, preventing swelling, discoloration, or strength loss even after 6+ months of storage.
Q3
Can this film be used for both frozen storage and high-temperature boiling sterilization?
Yes. Thanks to its high-temperature resistant polyethylene substrate with special cross-linking treatment, the film operates reliably across a temperature range of -20℃ to 121℃. It is suitable for frozen sauce storage as well as boiling sterilization processes at 121℃ for 10–30 minutes, with a heat-sealing strength attenuation rate of less than 5% during the process.
Q4
Does the IPE film meet international food safety standards?
Absolutely. All raw materials used in the IPE film comply with FDA (U.S. Food and Drug Administration) and EU 10/2011 food contact material standards. No harmful substances are released during acid-alkali resistance or high-temperature sterilization processes, making it fully safe for direct contact with food and sauces.
Q5
Is this film compatible with high-speed automated packaging lines?
Yes. The film features a high-flatness surface with thickness uniformity of ±2 μm, making it fully compatible with high-speed automatic packaging machines operating at 80–180 bags per minute. Its smooth conveying properties minimize jamming and reduce machine downtime, ensuring efficient and continuous production for food manufacturers.
Q6
Can custom branding or product information be printed on the IPE film?
Yes. The IPE film supports surface printing with an ink adhesion level of up to 4B, allowing food brands to customize logos, product names, nutritional information, and other visual elements directly on the packaging. This helps enhance brand recognition and improves the overall visual appeal of the packaged product on retail shelves.