request to quote
Leave Your Message

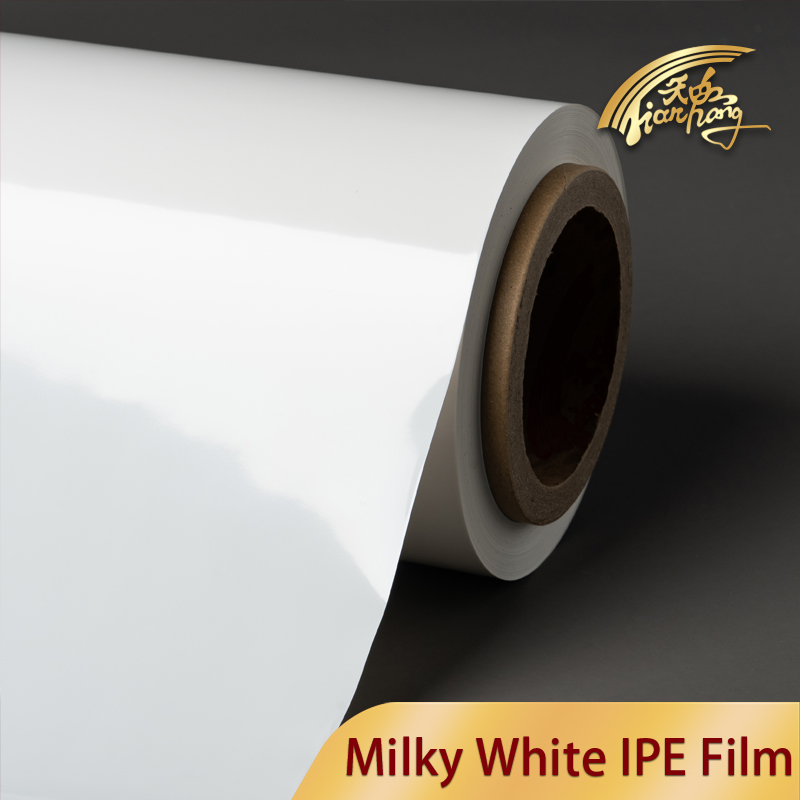
Milky White IPE Film - Pure White Polyethylene Packaging from China Suppliers & Factory for Food and Daily Necessities

,

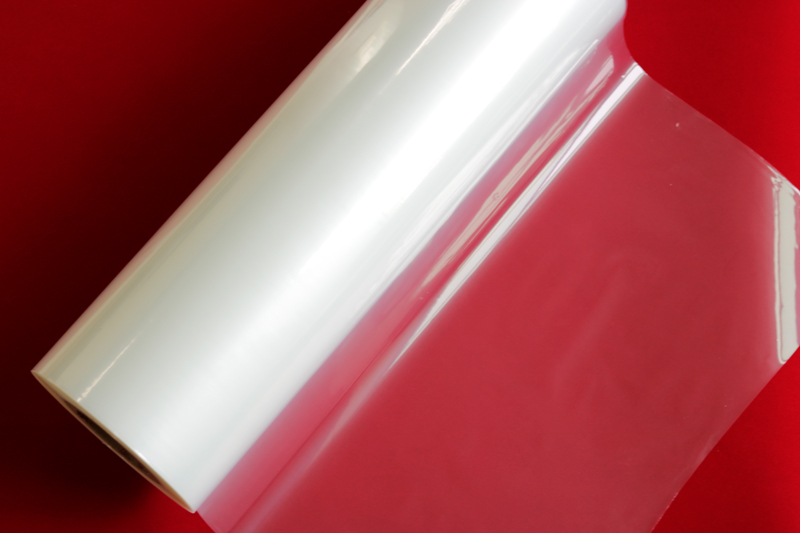
Color: White
Material: Polyethylene
Features: This packaging solution showcases a uniform milk-white color, providing a clean and attractive appearance. It boasts excellent light-shielding properties, protecting internal products from light exposure, along with basic protective features such as tensile resistance, puncture resistance, and a stable heat-sealing effect. Easy processing and forming make it versatile for various applications.
Application: Our polyethylene packaging is widely utilized in the food sector, including biscuits, candies, and dried goods. It's also perfect for daily necessities like tissues, wet wipes, washing powder and liquid detergent bags, as well as cotton soft towels and sanitary pads. This product is ideal for scenarios that require blocking product details or enhancing packaging texture. As a leading China supplier and factory, we specialize in providing high-quality polyethylene packaging solutions tailored to meet your business needs.

,

    Five-Layer Co-Extruded Blown Milk-White IPE Film
    🧪 1. Raw Materials and Appearance Advantages

    Utilizing high-quality milk-white masterbatch as the raw material ensures a uniform distribution of white color across the film, free from local color discrepancies or white spots, presenting a clean and full appearance. Moreover, the combination of high-grade raw materials and precise manufacturing processes stabilizes the film's physical properties, such as tensile and puncture resistance, resulting in minimal quality variations between batches.

    ⚙️ 2. Highlights of the Five-Layer Co-Extrusion Process Key Technology

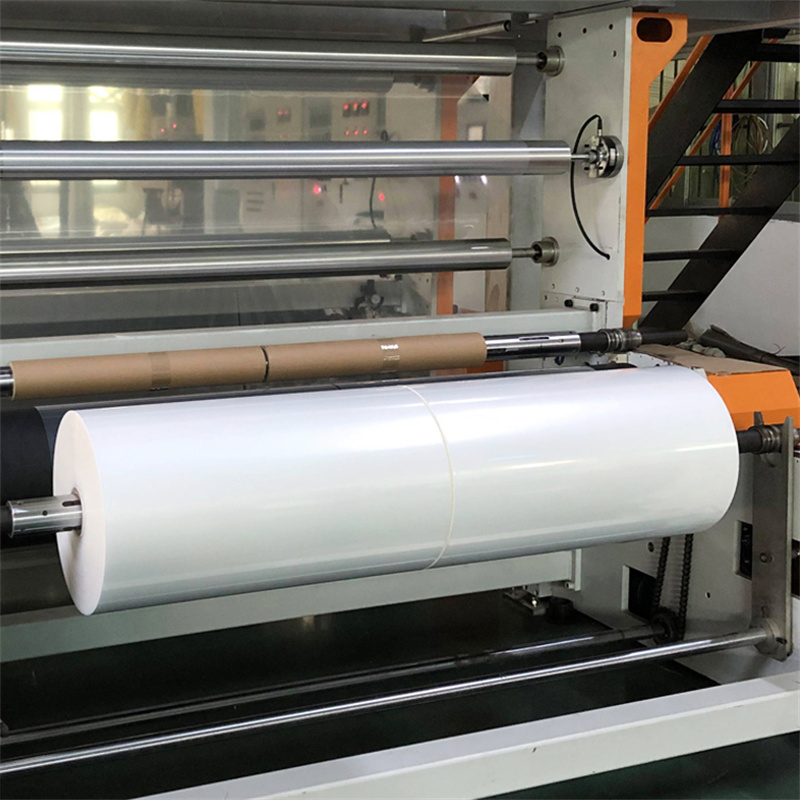
    Leveraging professional five-layer co-extrusion blow molding equipment, the milk-white functional layers can be co-extruded in a stratified manner. This design enables more precise control over the distribution density of the milk-white masterbatch. Compared with traditional processes, the resulting film exhibits higher whiteness and stronger covering power, effectively blocking external light and providing enhanced protection for the internal products.

    💰 3. Downstream Cost Savings and Heat Sealing Assurance Cost Benefit

    The high-quality milk-white film features a consistent and stable base color, allowing downstream flexible packaging manufacturers to directly print colorful patterns without the need for an additional white ink printing process. This significantly reduces production steps and cuts down on ink and labor costs. Additionally, when used in composite packaging, there is no requirement for white ink, eliminating the potential negative impact of white ink components on the heat sealing effect. This ensures a stable heat sealing temperature and improves the reliability of the package seal.

    🏭 4. Applicable Industries

    Widely applicable to industries with requirements for packaging light shielding, texture, and cost control, including the food industry (such as packaging for photosensitive and moisture-sensitive food items like biscuits, candies, dried goods, rice, and noodles), the daily chemical industry (such as packaging bags for daily chemical products like laundry powder, laundry liquid, dishwashing liquid, as well as packaging for hygiene products like cotton wipes and sanitary napkins), the home industry (such as packaging for household daily necessities like paper towels, wet wipes, and garbage bags), and can also be used for the protective packaging of certain light industrial products (such as small household appliance accessories and small tools).
    product-description1
    product-description2
    product-description3
    Frequently Asked Questions
    Q What makes five-layer co-extruded milk-white IPE film different from traditional single-layer white film?
    The five-layer co-extrusion process enables stratified distribution of milk-white masterbatch across multiple functional layers, resulting in significantly higher whiteness, stronger light-blocking coverage, and more consistent physical properties compared to traditional single-layer white film manufacturing methods.
    Q Can this film be directly printed with colorful patterns without pre-treatment?
    Yes. The stable and uniform base color of the milk-white film allows downstream flexible packaging manufacturers to print colorful patterns directly onto the surface, eliminating the need for an additional white ink printing process and reducing overall production costs.
    Q Does this film affect the heat sealing performance in composite packaging?
    No. Since the film's inherent white color eliminates the need for white ink in composite packaging applications, there is no interference from ink components on the heat sealing process. This ensures a stable heat sealing temperature and improves the reliability and consistency of the package seal.
    Q What industries and product types are best suited for this milk-white IPE film?
    This film is widely suitable for the food industry (biscuits, candies, dried goods, rice, noodles), the daily chemical industry (laundry products, dishwashing liquid, hygiene products), the home industry (paper towels, wet wipes, garbage bags), and light industrial product packaging (small appliance accessories and tools) — especially where light shielding, aesthetic texture, and cost efficiency are required.
    Q How consistent is the product quality between different production batches?
    Thanks to the use of high-grade milk-white masterbatch and a precise five-layer co-extrusion manufacturing process, the film maintains highly consistent physical properties — including tensile strength and puncture resistance — across different production batches, ensuring minimal quality variation for downstream manufacturers.
    Q How does this film help with light-sensitive product packaging?
    The five-layer co-extruded structure provides strong and uniform light-blocking coverage, effectively shielding packaged products from external light exposure. This makes it an ideal choice for packaging photosensitive and moisture-sensitive products such as food items, hygiene goods, and certain light industrial components that require protection from light degradation.

    Leave Your Message

    AI Helps Write