Leave Your Message
Explore our most sought-after film products designed to meet the rigorous demands of American food packaging, retail distribution, and industrial applications.
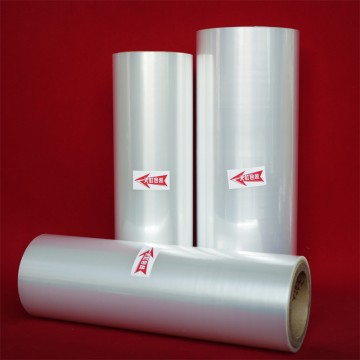
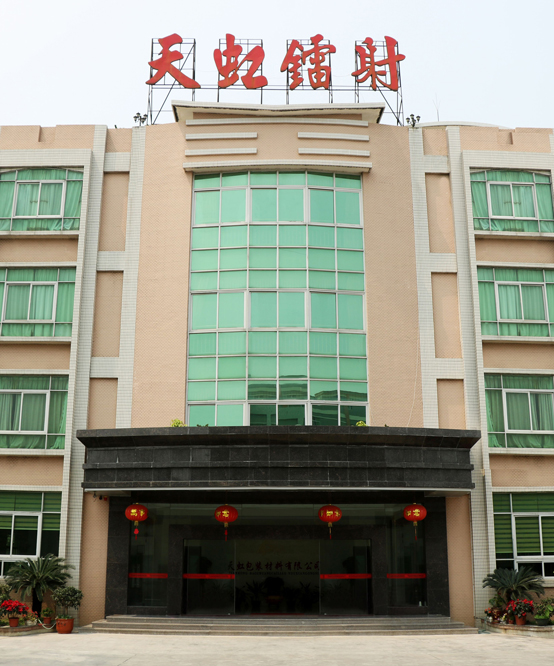
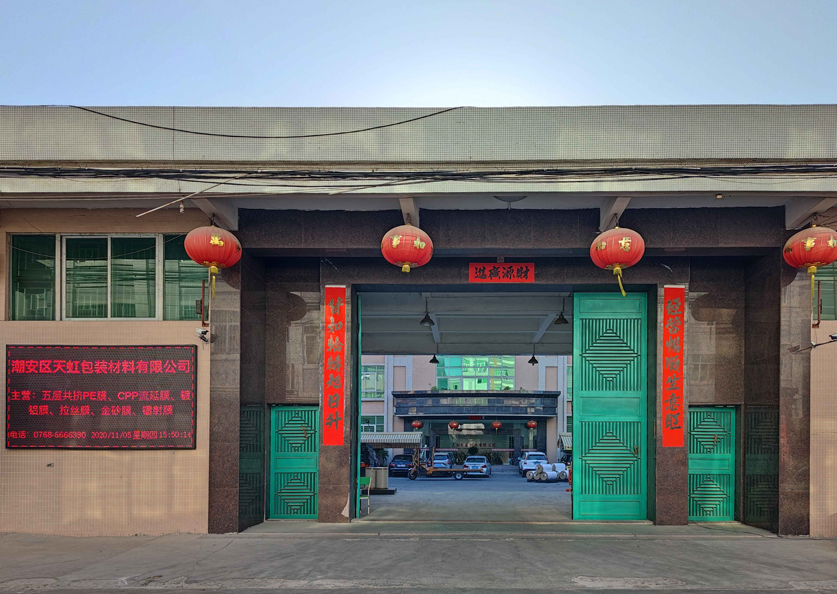
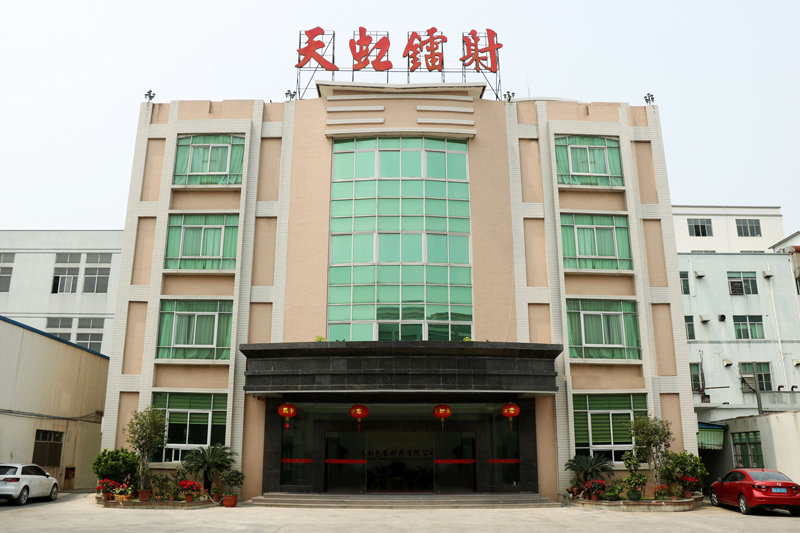
Chaozhou Chao'an Tianhong Packaging Materials Co., Ltd. has been deeply engaged in the plastic film industry since 1990, with over 30 years of experience in the R&D and production of high-performance films (CPP film, PE film, laser film, BOPET film, BOPP film, BOPA film, etc.). Located in Anbu Town, Chaoshan Plain, eastern Guangdong, China, the company is a comprehensive enterprise integrating the R&D, production, and sales of packaging materials.
As a leading film supplier, we are committed to providing core solutions for composite packaging substrates to color printing companies worldwide, covering the high-end packaging needs of various industries, including food, hygiene, pharmaceuticals, daily chemicals, and electronics.
The U.S. packaging film sector is one of the world's most dynamic markets, driven by innovation in food safety, sustainability mandates, and rapid e-commerce growth.
U.S. manufacturers across automotive, aerospace, and electronics sectors rely heavily on high-performance blast and protective films for surface protection during fabrication and transit, creating a multi-billion dollar annual demand for specialty films.
With U.S. e-commerce retail sales exceeding $1.1 trillion annually, demand for durable, printable, and anti-static PE and CPP films has surged across fulfillment centers from California to New York, driving rapid adoption of advanced film substrates.
American grocery chains including Walmart, Kroger, and Whole Foods Market demand anti-fog, high-clarity films for fresh produce and deli packaging. Anti-fog CPP and PE films are now standard across cold-chain logistics nationwide.
The U.S. pharmaceutical industry — the world's largest — requires FDA-compliant, high-barrier composite films for blister packs, pouches, and medical device packaging, pushing demand for precision-engineered film substrates.
California's SB 54 and federal extended producer responsibility (EPR) frameworks are reshaping U.S. film procurement. Brands now actively seek recyclable, biodegradable, and reduced-thickness films that meet both performance and regulatory requirements.
U.S. research institutions and film converters are investing heavily in nano-barrier coatings, biodegradable multilayer structures, and smart packaging films embedded with freshness indicators, positioning the market at the forefront of global packaging technology.
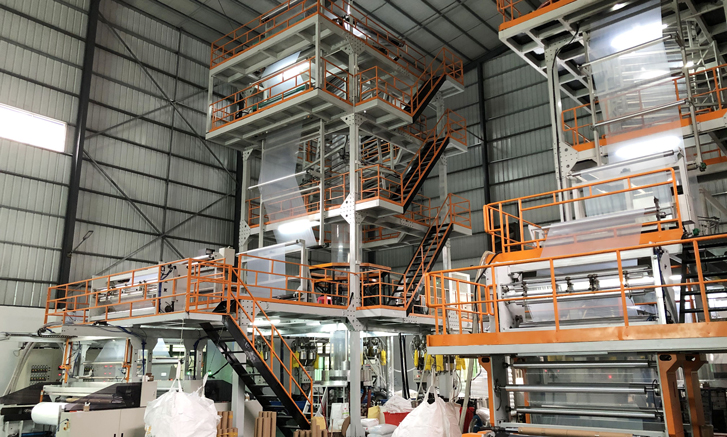
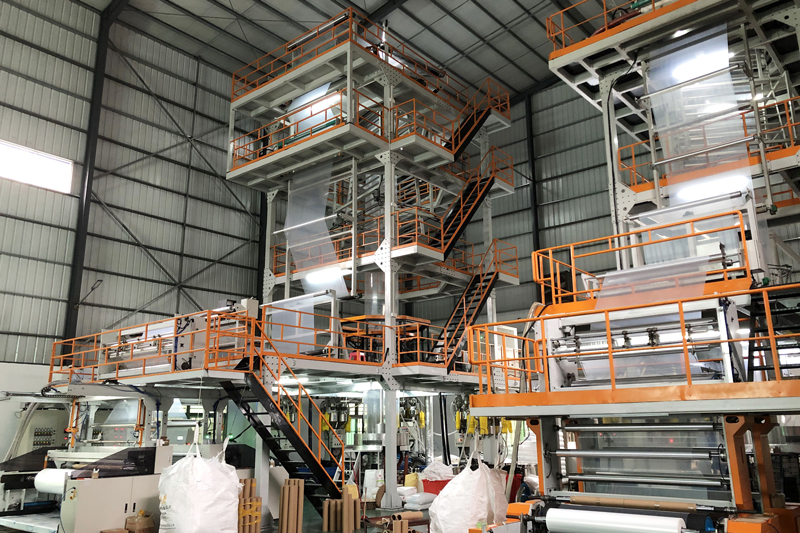
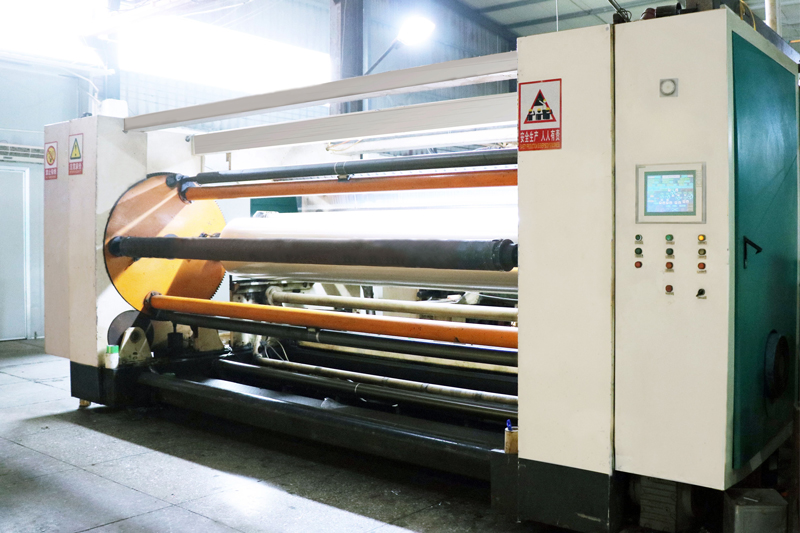
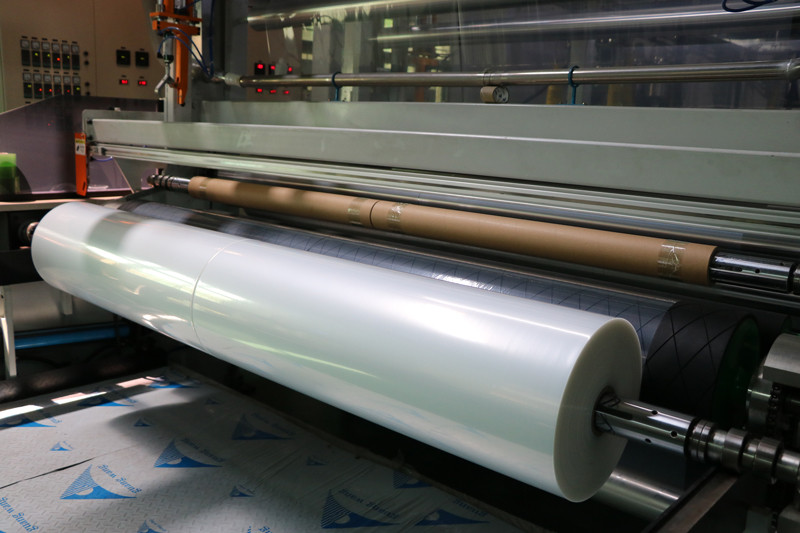
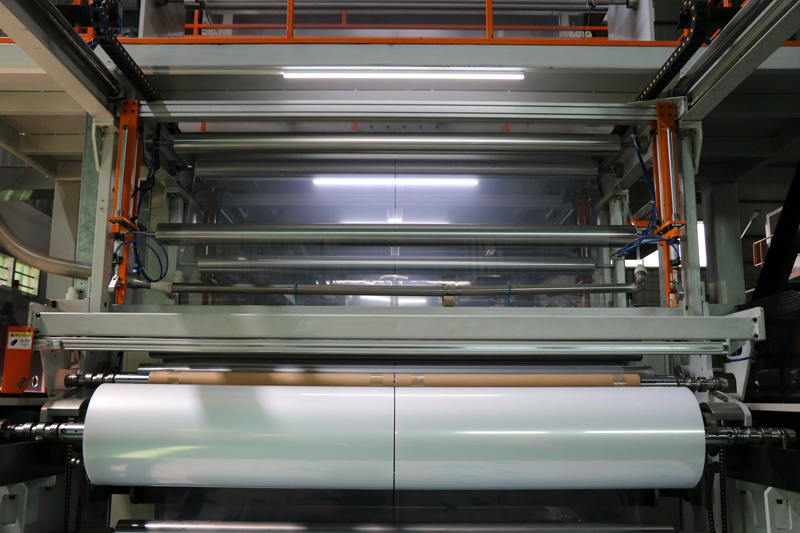
Our 50-acre modern production base is fully equipped with multiple five-layer coextrusion blow molding lines, CPP cast film lines, and wide-format laser lamination equipment. Combined with coating and embossing technologies, our annual production capacity reaches 20,000 tons.
Our technical team of nearly 100, including experienced R&D engineers, provides comprehensive support tailored to the specific needs of our clients' industries, including film selection, lamination process optimization, and functional development (such as antistatic and high-barrier properties), ensuring the optimal balance between packaging performance and cost.
Our unique laser and embossed films add a touch of vibrant color to laminated packaging, helping U.S. brands stand out on retail shelves across the country.
From sustainability legislation to smart packaging, these are the forces driving transformation in the American film and flexible packaging landscape.
U.S. brands are rapidly transitioning to all-PE and all-PP mono-material structures to meet How2Recycle labeling requirements and retailer sustainability commitments from Target, Amazon, and CVS Health.
Five- and seven-layer coextrusion lines are increasingly adopted by U.S. converters to deliver EVOH-based oxygen barriers without aluminum foil, enabling microwave-safe, transparent, and recyclable packaging for the American food market.
As U.S. food manufacturers invest billions in automated packaging lines, demand for films with consistent slip, COF, and seal-initiation-temperature properties has intensified, requiring tighter production tolerances from film suppliers.
Driven by consumer demand and state-level composting infrastructure, PLA and PBAT-based compostable films are gaining traction in U.S. foodservice, farmers' markets, and natural grocery channels, creating new opportunities for innovative film producers.
The U.S. premium food, spirits, and cosmetics sectors are driving demand for laser-embossed and holographic films that deliver shelf differentiation, brand authentication, and anti-counterfeiting features in a single substrate layer.
U.S. retailers and CPG brands are mandating film lightweighting initiatives to reduce material costs and carbon footprints, pushing film manufacturers to develop thinner yet stronger film structures through advanced coextrusion and nano-additive technologies.
Our films serve a wide spectrum of American industries — from coast-to-coast grocery chains to Silicon Valley tech packaging and Midwest agricultural distribution.
Anti-fog PE films used by U.S. meat processors and supermarket deli counters to maintain product visibility and extend shelf life in refrigerated display cases.
High-speed CPP and BOPP films powering automated packaging lines at American snack brands — from potato chips in Ohio to artisan chocolates in Vermont.
Laser and embossed films used by U.S. beauty brands for premium laminated pouches, sachets, and retail packaging that command premium shelf positioning.
High-barrier composite films for unit-dose pharmaceutical pouches, meeting FDA 21 CFR requirements for direct-contact drug packaging across U.S. contract manufacturers.
Heavy-duty PE films serving U.S. agricultural operations in California's Central Valley and the Midwest for silage wrapping, greenhouse coverings, and produce protection.
PE sealing films for milk tea, yogurt cups, and fast-food beverage lids — increasingly demanded by U.S. bubble tea chains and QSR operators coast to coast.
Durable, puncture-resistant PE film bags and pouches used in Amazon, Shopify, and DTC fulfillment centers for protective product packaging and void fill applications.
Antistatic and clean-room-grade films protecting semiconductors, PCBs, and precision components during manufacturing and shipping at U.S. tech facilities.
"Committed to serving global flexible packaging color printing companies, using innovative film materials to drive the transformation of packaging towards green, efficient, high-barrier, and high-quality."
Tianhong will continue to invest in R&D, focusing on cutting-edge fields such as high-barrier composite substrate films, biodegradable materials, environmentally friendly laser films, and embossed films, helping our clients seize opportunities in the wave of sustainable development.
For U.S. partners, we offer dedicated technical consultation, sample programs, and customized film development services aligned with American market standards, regulatory requirements, and brand specifications. Contact us to collaborate on developing innovative and efficient packaging solutions for your American business.
Our 50-acre production base in Guangdong, China is equipped with state-of-the-art coextrusion, casting, and lamination lines — delivering consistent quality to U.S. customers at scale.
Partner with Tianhong — 30+ years of film manufacturing expertise, 20,000-ton annual capacity, and dedicated support for American market requirements.
Request a Sample or QuoteFrom anti-fog PE films to cup sealing solutions — explore our complete portfolio engineered for American food, beverage, pharmaceutical, and industrial applications.